Stainless Steel Sphere Sculpture & Mirror Ball Water Feature: A Complete Guide
September 23, 2026
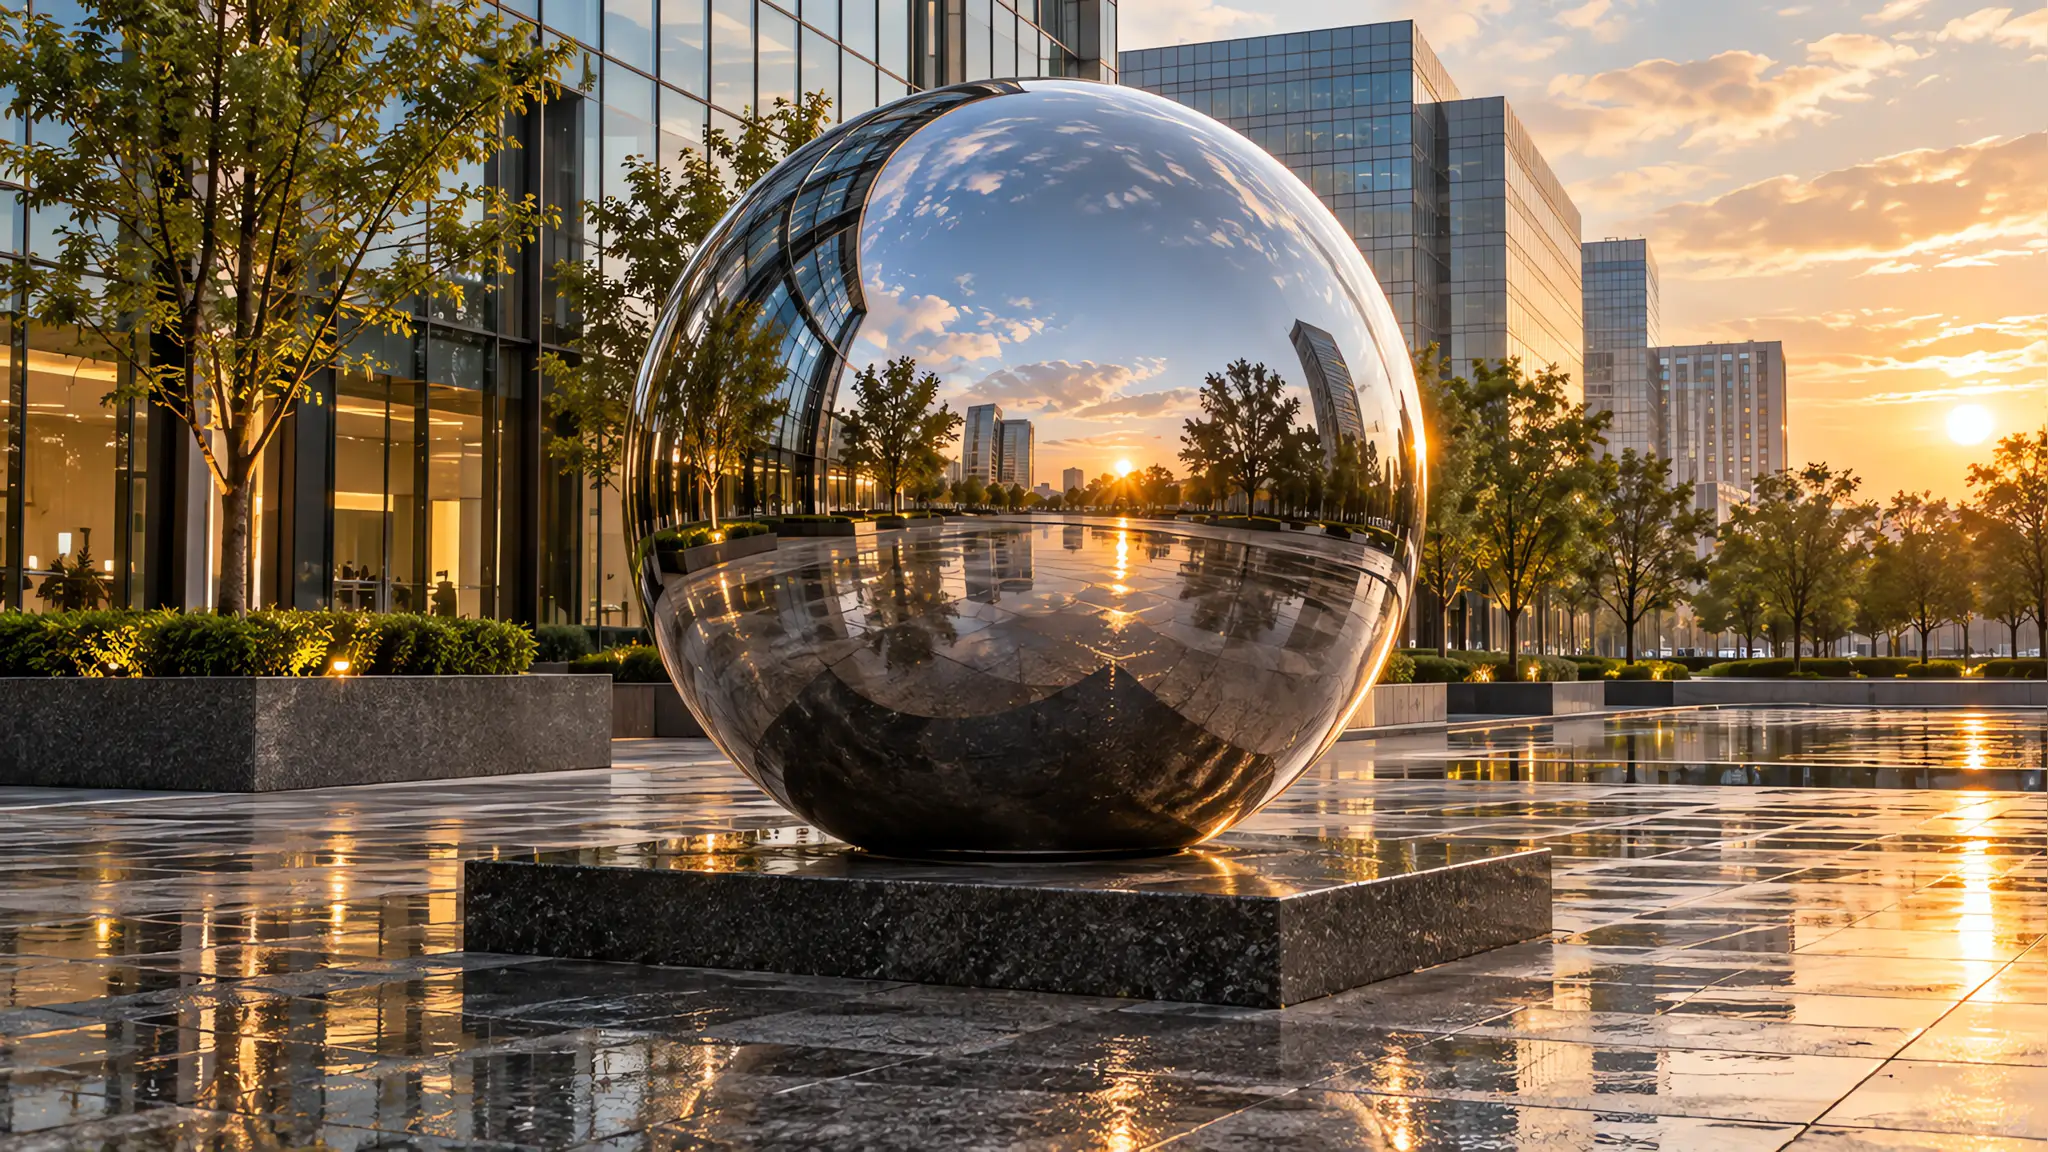
A mirror-polished stainless steel sphere is the least forgiving form a fabricator can be asked to make. There is no flat panel to hide a weld, no facet to break up a reflection, no shadow to disguise a wave. Every square centimetre reflects at full strength, so every square centimetre is a magnifying glass pointed at the workmanship.
A 2 m stainless steel ball sculpture can cost several times a 2 m abstract form while using less material. This guide covers how a true sphere is formed, how a sphere water feature is engineered, how to site one, and where the cost sits.
Why the Sphere Is the Hardest Form to Fabricate
- Curvature magnifies every defect. A 0.2 mm wave is invisible on a flat panel; on a 2 m sphere it distorts the reflected horizon across a visible band.
- No seam can hide. A weld on a rectangular form can hide in a shadow line; the equator weld of a sphere runs around its most visible part and must vanish after polishing.
- Roundness is unforgiving. A 2 m sphere out of round by 3 mm is 99.85% correct, yet the eye reads it as an egg.
So a sphere concentrates almost all its cost in labour, not material: the sheet is cheap, the forty to sixty hours of welding, grinding and polishing are not.
How a True Sphere Is Formed
The route is chosen almost entirely by diameter.
Spun hemispheres
Up to about 1.2 m, a flat stainless disc is spun over a former on a lathe into a hemispherical shell with no welds in the bowl and a wall that thins toward the pole by 8–12%. It is the default for small spheres.
Pressed hemispheres and gores
Above 1.2 m, hemispheres are pressed from flat sheet in matched dies or formed in segments. Spheres of 3 m and larger are usually built from six to twelve gores — curved panels shaped like orange segments — because no press can form a 1.5 m deep dish in one hit.
The welded equator and the polish sequence
The equator seam is the critical joint: a full-penetration TIG weld, back-purged with argon so the inside does not oxidise and sugar, dressed flush outside. On gore-built spheres the seams converge at the poles, so the pole is a second critical zone, often finished as a machined cap.
Making the seam disappear is staged: coarse grinding to remove the weld crown, then progressively finer abrasives — 120, 240, 400, 800, 1200 and 2000 grit — then buffing. Each stage must fully erase the previous scratch pattern; skip a grade and the scratches only surface once the metal is bright, forcing the sphere back two grades. This is the most common cause of a sphere project running over programme: process discipline, not material cost, decides the outcome.
Wall Thickness and Internal Armature
A sphere is efficient in uniform compression but poor locally: an unsupported shell flattens under its own weight and oil-cans as wind pressure changes.
- Wall thickness. 1.5 mm suits spheres up to about 1 m; 2–3 mm for 1–2 m; 3–4 mm for 2–3 m; 4–6 mm or a designed internal structure beyond that. Thicker sheet resists denting and holds roundness during polishing, but doubling wall thickness roughly doubles shell weight and material spend.
- Internal armature. Anything above about 1.5 m should carry an internal frame — hub-and-spoke or ring stiffeners welded to the inner shell — carrying weight to the base and resisting local deflection. On a water feature it also supports the weir and pipework, so it is designed with the hydraulic layout, not after it.
What “Mirror” Actually Means in Practice
Mirror finish is a grade, not a switch, and the difference is visible from across a plaza.
- Brushed or satin (No. 4 / hairline). A directional grain, forgiving of minor surface variation and much cheaper; reflections are blurred and the surface reads as soft metal.
- Standard polish. Reflective but with visible image distortion — for a general sheen rather than a true reflection.
- Mirror polish. A near distortion-free reflection from a very fine compound; this is what clients picture when they say “mirror”, and where the labour cost sits.
- Super-mirror or optical grade. For spheres where a clean reflected image is the entire point — but each extra grade multiplies inspection time.
Our guide to stainless steel sculpture finishes sets the grades out side by side.
Sphere Water Features: The Weir Overflow Detail
A sphere water feature is a mirror sphere with water flowing over it in a uniform film, and almost all the engineering lives in the weir — the lip over which water is released onto the curved surface.
A chamber at the crown is fed by the pump, with a machined lip following the sphere’s curvature. Water spills over that lip and clings to the surface as it runs down to a catch basin. The lip must be levelled to within a fraction of a millimetre: a 1 mm variation around the circumference breaks the film into channels and leaves dry streaks on the mirror. The weir is often a separate machined ring, trial-fitted before assembly.
Pump and reservoir sizing
Film flow scales with wetted circumference, not a pump’s headline figure: plan 1.5–2.5 litres per minute per metre of wetted circumference for a thin, quiet film. The catch basin must cover the pump intake with margin plus a reserve for evaporation and splash — typically a 3 to 5 minute buffer at operating flow. Filtration and level control are effectively mandatory in public work.
Water film uniformity
Uniformity is a joint product of the weir lip and the sphere surface. The surface must be free of polishing residue, oil and wax: invisible when dry, they make the film bead and channel within hours. And the film is only as even as the geometry beneath it, so the roundness tolerance above is hydraulic, not cosmetic. Full hydraulic detail is in our guide to stainless steel water feature engineering.
The reward is that the feature reads as one continuous surface: the moving film hides fine polishing marks and blends the equator seam into an unbroken reflection.
Siting: Scale, Plinth, Base and Wind Loading
- Scale and plinth. The plinth should read as subordinate — commonly 0.3–0.5 times the sphere diameter in height and at least 0.8 times in width, so the sphere appears to float rather than balance.
- Base connection. A sphere is anchored through a machined spigot or recessed seating ring, with a drainage weep so water cannot pool and stain the base.
- Wind loading. A sphere has a high drag coefficient (around 0.5) and presents the same frontal area from every direction, so it cannot be oriented to shed wind; uplift on the anchor often governs rather than overturning. Our article on wind loading for large stainless sculptures sets out how base geometry is sized.
- Anti-rotation. A free-spinning sphere is a liability in public space: it invites handling and will be set spinning by wind. Specify a locked or keyed connection unless rotation is a deliberate feature.
304 vs 316 for Coastal and Chlorinated Sites
Grade selection is decided by the environment, not the budget. Grade 304 is the workhorse and is entirely adequate inland, away from salt and chlorinated water. Grade 316 adds molybdenum, which markedly improves resistance to chlorides, and is the correct choice for coastal sites, for any sphere in contact with chlorinated pool water, and where de-icing salt is used. A mirror finish amplifies the consequences of the wrong choice, because tea-staining and pitting are far more visible on a bright surface. Our comparison of 316 versus 304 stainless steel for outdoor sculpture covers the exceptions and passivation requirements, and the 316 stainless material page lists what we fabricate in.
Maintenance Reality for a Mirror Sphere
- Frequency. Inland and sheltered, a wash and dry every 6–12 weeks keeps a good surface; coastal, urban or high-traffic sites need it every 2–4 weeks. Rain does not clean a sphere — it leaves mineral spotting that etches if left.
- Method. Non-abrasive neutral cleaner, soft microfibre, and a final rinse with deionised water where water is hard; abrasive pads and acid cleaners destroy the polish permanently.
- Water features. Add filtration checks, a seasonal descale of the weir lip and a water treatment regime; biofilm is the main enemy of a bright surface.
- Damage. A scratch on brushed metal can often be blended out on site; on a mirror sphere it usually needs local re-polishing, and a deep one may mean returning the sphere to a workshop — the strongest argument for keeping a mirror sphere out of public reach.
Cost Drivers and Typical Ranges
A large mirror sphere is one of the most expensive forms per square metre of surface, for arithmetic rather than markup reasons: surface area is small relative to the hours needed to make it flawless. A 2 m sphere has about 12.6 m² of surface and can absorb 150–250 hours of skilled finishing; a flat 12.6 m² panel absorbs a small fraction of that.
The main cost drivers are diameter, finish grade, wall thickness and armature, water feature complexity, stainless grade and site access. A 1 m sphere runs roughly USD 8,000–20,000; a 2 m sphere USD 25,000–60,000; and a 3 m sphere USD 70,000–160,000, with mirror grade and gore construction at the top of each band. For a breakdown of what moves a sculpture budget, see our stainless steel sculpture cost guide.
Decision Table: Which Sphere Specification Fits?
| Specification | Best for | Surface | Indicative cost (2 m) | Watch out for |
|---|---|---|---|---|
| Mirror sphere (static) | Feature plazas, entrances, hotel forecourts, interiors | Mirror polish, near distortion-free | USD 30,000–60,000 | Scratches are permanent defects; needs regular cleaning |
| Brushed sphere | Landscape schemes wanting a softer read | No. 4 / hairline grain | USD 18,000–35,000 | Grain must be consistent or it reads patchy |
| Sphere water feature | Pool terraces, courtyards, hotel lobbies | Mirror or satin under a water film | USD 45,000–90,000 | Weir lip tolerance is critical; filtration is mandatory |
| Static ball on a plinth | Public art, memorials, gateways, coastal markers | Mirror, brushed or patinated | USD 32,000–70,000 | Wind uplift often governs the anchor; anti-rotation needed |
Browse the sphere sculpture range to see these options on real projects, and the water feature range for moving-water installations.
Have a project in mind?
A sphere is a specification where the early decisions — grade, finish, wall thickness, weir tolerance and base connection — determine whether the finished object reads as a flawless mirror or a slightly wobbly ball. Send us the diameter, setting and finish you have in mind and we will come back with a feasibility note and an indicative cost range. Request a quote and we will tell you honestly what the form will and will not do at your scale.
More from the Workshop
Have a Project in Mind?
Send your brief and get a free, honest quote within 24 hours — no obligation.
Request a Quote